Hey folks,
If you’re in pharma packaging, you know cartoning machines aren’t just boxes that fold and close — they’re the last line of defense before your meds hit pharmacy shelves. Let’s cut to the chase: I’m a drug cartoning machine supplier, and 9 out of every 10 buyers I talk to skip over the data-logging part when they’re vetting new gear. Big mistake. Most of us assume “logging” is just a timestamp of when a box closed, but today I’m breaking down what a modern drug cartoning machine actually logs, why it matters, and how it’ll save you headaches (and maybe your audit score) down the line. Drug Cartoning Machine
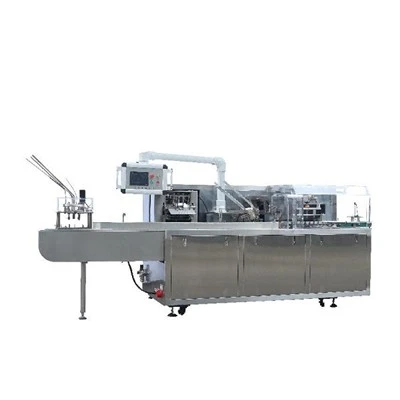
First, let’s get one thing straight: this isn’t the 2015 version of a cartoner. Old-school machines spit out a basic printout of total cartons run, but today’s systems? They’re basically little industrial data hubs, and the best ones sync straight to your QMS (Quality Management System) software — no manual data entry, which is a win in a space where even a single typo can trigger a 48-hour FDA audit stop.
Let’s start with the core, non-negotiable logs. First up: individual carton traceability. Yeah, that serial number or lot number you print on each box? A good cartoner doesn’t just print it — it logs every single one, linked to the machine’s exact run time, batch ID, and even the position of the carton on the conveyor. Wait, you run a batch of 10,000 500mg amoxicillin boxes? If a vial upstream (like a blister pack machine) has a bad dose, you don’t have to recall every box from that shift. You can pull every log entry for that serial number, cross-check it to the blister pack’s logs, and narrow the recall to just the 120 bad cartons. No one wants to field calls from pharmacy managers panicking about recalls, trust me.
Next, machine performance data. I’m talking cycle rate — how many cartons it’s cranking out per minute, not just an average. If it dips from 120 cpm to 90 cpm mid-run, the log will flag that, plus tell you why: maybe a glue roller was running dry, or a carton blank got warped from humidity. A lot of suppliers frame this as “OEE data,” but let’s keep it real: OEE (Overall Equipment Effectiveness) logs aren’t just for our maintenance team. Your production manager can use the logs to schedule downtime before a small issue becomes a 2-hour line stop. I’ve had a client who caught a misaligned feeder via log data last quarter — saved them $18k in lost production that week alone.
Then there’s quality-critical logging, which is where most people trip up. Modern cartoners have cameras and sensors that check for missing inserts (like patient info booklets), wrong lot numbers, or crimped flaps. Every time the camera rejects a bad carton, that event gets logged with a timestamp, the reason for rejection, and even a snapshot of the bad carton. Think about it: if an audit asks “how many defective cartons did you run in the last 30 days?” you don’t have to dig through a stack of reject bins. You pull the machine’s log, run a quick filter, and boom — instant report. No messy manual counts, no discrepancies that lead to audit findings.
Wait, what about environmental and process data? I know, it’s extra, but it’s game-changing. Some of our top-tier machines log the temperature of the glue system, the humidity of the machine’s enclosure (super important if you’re handling sensitive biologic cartons), and even the pressure of the carton forming rollers. Why? If you’re packaging a product that requires a specific glue cure time, the log will show if the glue temp dropped too low mid-run, which would lead to flaps popping open later. That’s not a “machine error” — that’s a preventable quality issue, and the log gives you proof you caught it before it reached the warehouse.
But here’s the thing: not all data logging is created equal. A lot of cut-rate machines will sell you “data logging” as a throw-in feature, but it’s just a basic CSV file that you have to manually download every shift. The good stuff? It’s cloud-integrated (secure, obviously — we use HIPAA-compliant servers for our clients) so you can pull logs from your office, or even your phone, during a site visit. It also lets you set alerts: if reject rates spike above 0.5% (which is the pharma industry standard), you get a text or email, not just a 2AM log entry waiting in your inbox. That’s the difference between a machine that’s a tool and one that’s a proactive partner.
Now, let’s talk use cases that most suppliers don’t highlight. Last year, a vaccine manufacturer I work with needed to track cartons that were labeled for cold chain compliance. Their cartoner logs tagged every carton with the exact time it exited the machine and was loaded into a temperature-controlled truck. When the FDA asked for proof that vaccines never left the 2–8°C window during packaging, they pulled the carton logs, cross-referenced with the truck’s GPS, and passed the audit in 10 minutes. Another client makes pediatric meds, and their logs track which cartons went to pediatric clinics vs. adult pharmacies — so when there’s a recall on a kids’ dose, they only notify the 120 clinics instead of 500 retail locations. That’s the kind of specificity you can’t get from a basic old machine.
But let’s be honest: there are limits, and I don’t sugarcoat this. Data logs don’t fix bad machine design — if your cartoner jams 10 times an hour, the logs will show you how many jams, but you still need a machine that’s built for pharma reliability. Also, you have to make sure the logging system is GxP-compliant if you’re in regulated markets (US, EU, Japan, etc.). That means no tampering with logs, audit trails that can’t be altered, and timestamp sync that’s accurate to within a second. A lot of cheap logging systems let operators edit log entries, which is a red flag for audits. All our machines have lockable logs — only your quality team can export or edit them, and every change is logged separately.
Here’s why I’m passionate about this: I’ve seen too many pharma teams waste weeks dealing with audit delays, recall missteps, and lost production because they bought a cartoner that only did “basic” functions. When a client comes to me asking about data logging, I don’t just list features — I walk them through their specific pain points. If they’re a small biotech doing 10,000 unit runs a month, they don’t need a $50k cloud system. If they’re a large manufacturer doing 1M unit runs a week, they need real-time sync and alerting.
Now, if you’re shopping for a new drug cartoning machine (or upgrading your current one), don’t just ask “does it log data?” Ask these specific questions:
- Can I trace every individual carton to its lot/serial number and production shift?
- Does the logging system integrate with my QMS or ERP, or do I have to manually import data?
- Are logs tamper-proof and GxP-compliant for regulated audits?
- Can I set real-time alerts for reject rates, cycle drops, or environmental issues?
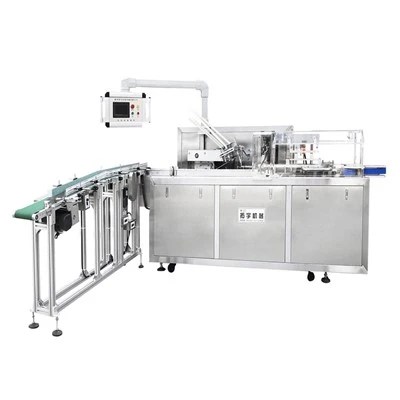
At the end of the day, your cartoner’s data logging isn’t just a feature — it’s a way to de-risk your packaging line, save time during audits, and make recalls way less stressful. I’ve helped dozens of pharma teams pick machines that fit their logging needs, so if you’re tired of dealing with old, finicky cartoners that leave you flying blind on data, reach out to me to chat through your specific setup. We can walk through exactly what your line needs, no sales pitch, no jargon, just straight talk.
Drug Bagging Machine References
- U.S. Food and Drug Administration. (2022). Guidelines for Pharmaceutical Packaging Automation and Data Integrity Requirements.
- International Society of Pharmaceutical Engineering (ISPE). (2023). Data Logging Best Practices for Continuous Pharmaceutical Manufacturing.
- Pharmaceutical Packaging Association. (2022). Recall Mitigation Strategies Using Cartoning Machine Traceability.
Zhejiang Tuoyu Packaging Machinery Co., Ltd.
Zhejiang Tuoyu Packaging Machinery Co., Ltd. is one of the most professional drug cartoning machine manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale durable drug cartoning machine made in China here from our factory. Good service and quality products are available.
Address: Workshop No.12, No.11-19, Xinbin Road, Binhai New Area, Pingyang County, Wenzhou City
E-mail: 15868789201@163.com
WebSite: https://www.tuoyupack.com/
