If you’re reading this, chances are you’re either a small-batch puffed snacks producer hitting a wall with inconsistent product quality, a mid-sized facility looking to scale without ruining your signature crunch, or maybe someone who just bought their first puffed snacks processing machine and is staring at a confusing control panel wondering what all those dials and buttons actually do. I’ve been there—back in 2012, I was a field service tech for a puffed snacks processing machine supplier, crawling into back factories at 2 a.m., fixing machines that’d gone haywire mid-production, and learning that 90% of the time, the problem wasn’t a broken part—it was a parameter that’d been tweaked wrong. Now, after 12 years of working with producers across 17 countries, I still get calls every week from people asking how to adjust their machine settings to get the exact puffed snack they want: light and airy puffed rice sticks, dense and chewy corn puffs, crunchy potato chips, all without wasting half a batch or calling an emergency tech. Let’s break this down, no jargon, no textbook fluff, just real, hands-on advice I’ve seen work in thousands of production lines. Puffed Snacks Processing Machine

First, let’s set the baseline: every puffed snacks processing machine is a series of linked steps that build on each other. You can’t adjust the final puffing pressure without fixing the moisture content of your raw grain first—start at the beginning, or you’ll end up chasing your tail. I always tell new producers to do a “dry run” first: load the machine with just the raw grain (no seasonings, no oil, nothing extra) and run it through a short cycle, writing down every reading: grain moisture level, barrel temperature, screw speed, die pressure, and the final product’s texture. That baseline is your benchmark. If you don’t know how your machine performs when it’s on default settings, you’ll never know what to change. I once worked with a small producer in rural Indiana who’d been running his corn puffs at 180°C barrel temperature for months, wasting 20% of his batch, because he’d never done a dry run—his default was actually set to 170°C, and he’d been tweaking a parameter that didn’t need to be touched at all.
Let’s start with the most foundational parameter: moisture content of the raw grain. This is non-negotiable. Puffing works because when you heat a grain with trapped moisture, the water turns to steam, expands, and pushes the grain’s starch structure outward. If your grain is too dry, there’s not enough steam to create a puff—your product will be dense, hard, and maybe even crumbly. If it’s too wet, the steam will expand too early, before the starch has set, and you’ll get flat, soggy puffs that break apart mid-packaging. Most producers don’t realize that grain moisture fluctuates with humidity, even if you store it in a sealed bin. A humid summer day can add 2% moisture to your grain overnight, which means you need to adjust your machine parameters that day too. The sweet spot for most puffed snacks is 12-16% moisture in the raw grain. How do you adjust this? Don’t overcomplicate it: if your puffs are too small and dense, add a tiny bit of water to your grain mixer (1-2 teaspoons per kg of grain, no more) and run a test batch. If they’re too airy and break easily, let the grain sit out for an hour to lose a bit of moisture, or adjust the barrel’s drying zone to pull extra moisture out before heating. I once had a customer in Thailand who’d been importing grain stored in sea containers, which had 19% moisture during monsoon season—his puffs were so flat they wouldn’t fit in standard bags. We spread the grain out on a concrete floor for 45 minutes, and added 0.5% of maltodextrin to the mix to bind the extra moisture, and his puff volume doubled without him having to buy a whole new machine. That’s the kind of small, cheap adjustment that makes all the difference.
Next, screw speed in the extruder barrel. The extruder is the heart of your puffed snacks machine—this is where the raw grain is mixed, heated, and forced through the die to form the shape of your snack. Screw speed controls how long the grain is in the barrel, how much pressure builds up, and how well it’s mixed. If screw speed is too low, the grain sits in the barrel too long, overheats, burns, or turns into a sticky mess that clogs the die. If it’s too high, the grain doesn’t get enough time to mix evenly, so some parts are too dry, some too wet, and your final product will have inconsistent texture—one bite crunchy, the next chewy. For most standard puffed snacks (corn puffs, rice cakes), a screw speed of 200-300 RPM works. For denser, chewy snacks like puffed wheat sticks, drop it to 150-200 RPM, so the grain gets more time to set before exiting the die. For extra light, airy snacks like cheese puffs, bump it up to 300-350 RPM to build more pressure that will expand when the snack exits the machine. Pro tip: don’t adjust screw speed alone—always pair it with barrel temperature. If you crank up screw speed to get faster production, you’ll need to lower barrel temperature by 5-10°C, because more friction from faster screws creates extra heat that can burn the grain. I learned this the hard way when I tested a machine at a trade show once—cranked screw speed to 400 RPM, forgot to lower the barrel temp, and ended up with a batch of charred corn that smelled like burnt popcorn and turned the trade show booth gray. Don’t be me.
Then there’s barrel temperature, split into three zones: feed zone, mixing zone, and heating zone. The feed zone is where the grain first enters the barrel—this zone should be cool, around 30-50°C, to start softening the grain without cooking it too early. If the feed zone is too hot, the grain will start cooking before it’s mixed, leading to clumps. The mixing zone is where the grain is blended with water, oil, or seasonings, and where starch gelatinizes (that’s what makes the puff structure stable). This zone should be 80-120°C, depending on your grain. For corn, I usually set it to 90°C; for rice, 105°C; for wheat, 110°C. The heating zone is the final zone before the die, where pressure builds and steam forms to create the puff. This is the most variable zone, and where most producers mess up. If your puffs are under-puffed, too dense, or have a raw, starchy taste, crank this zone up by 10-15°C. If they’re over-puffed, too airy, or have a hollow, fragile structure, lower it by the same amount. A mistake I see all the time is producers setting the heating zone too high, trying to get bigger puffs, which actually makes the steam expand too fast, tearing the starch structure and leaving you with puffs that pop or break during packaging. Last year, I worked with a snack brand that was rejecting 15% of their cheese puff batches because they were breaking on the packaging line. We dropped the heating zone from 180°C to 165°C, and the breakage rate dropped to 2%—no new parts, no extra cost, just a 15°C tweak.
Die pressure is the next critical parameter, and it’s directly tied to barrel temperature and screw speed. The die is the plate at the end of the extruder with small holes that shape your snack—pressure here is what forces the molten grain through the holes, and when the pressure is released as the snack exits the machine, that’s what makes it puff. Die pressure is measured in bar (PSI, for US producers), and for most puffed snacks, it’s between 10-20 bar. How do you adjust it? Die pressure goes up when you lower the die hole size, increase screw speed, or raise barrel temperature. It goes down when you widen die holes, lower screw speed, or lower barrel temp. If your snack isn’t holding its shape after exiting the die, die pressure is too low—try raising it by 2 bar at a time, until the shape is consistent. If your snack is getting stuck in the die or is irregularly shaped, die pressure is too high—drop it 1-2 bar. I once had a customer making mini puffed balls for a cereal mix, and his balls were coming out deformed, half flat, half round. We measured his die pressure and it was 22 bar—way too high for the tiny die holes he was using. We swapped to slightly larger die holes and lowered pressure to 16 bar, and his balls were perfect. Simple fix, but it took him 3 months to figure out because he was only adjusting barrel temp, not die pressure.
Then there’s the dryer section, which is often overlooked by new producers, but it’s what gives your puffed snack its final crunch and shelf life. After exiting the extruder, your snack has around 15-20% moisture, which is way too high to package—if you put it in a bag right away, it’ll go soggy in 24 hours. The dryer removes that extra moisture, bringing the final moisture content down to 8-12%, which is ideal for crispness and storage. Dryer parameters are temperature and air flow. If your snack is soggy and chewy after drying, your dryer temperature is too low, or air flow is too weak—crank dryer temp to 100-120°C for 5-10 minutes, or increase air speed to pull more moisture out. If your snack is burnt on the outside but still chewy on the inside, dryer temperature is too high, or you’re drying for too long—lower temp to 85-95°C, and cut drying time by 2 minutes. Another common mistake: producers run the dryer at full speed 24/7, but if you’re producing smaller batches, you can lower dryer speed, which saves energy and reduces the chance of burning the snack. I had a small bakery that started making puffed snacks as a side product, and their electricity bill jumped 30% after buying a puffed machine. We adjusted their dryer to run only when snacks were passing through, and their bill went back down without affecting quality.
Now, let’s talk about how to adjust these parameters step by step, so you don’t have to guess. First, do a test run with no seasonings, no oil, just raw grain, as I mentioned earlier. Take 10 sample snacks from the exit of the machine, let them cool for 2 minutes, and test them: texture (crunchy, chewy, dense, airy), shape consistency, and shelf life (leave one on a counter for an hour to see if it gets soggy). Then, adjust one parameter at a time—never tweak two settings at once, or you’ll never know which change fixed the problem. For example, if your puffs are too dense, first check grain moisture—if it’s 12%, move to screw speed: if it’s set to 200 RPM, bump it to 250 RPM. Run a test batch, check the texture. If it’s still too dense, then adjust heating zone temp, not both screw speed and temp at the same time. I can’t stress this enough—adjusting only one variable at a time is the number one rule of parameter tuning. If you change screw speed and barrel temp together, and your puffs get better, you have no idea which one was the reason, and you’ll have to re-tune every time you switch grain types (corn vs. rice vs. wheat).
Also, don’t forget about raw grain variability. Different grains have different starch contents, which affect how they puff. Corn has high starch, so it puffs more easily—you can get away with lower barrel temp and lower screw speed. Rice has lower protein and higher starch, so it needs a slightly higher heating zone temp to puff properly. Wheat has more protein, so it needs higher screw speed and more mixing time to break down the protein structure. If you switch grain suppliers, that’s a sign to re-do your parameter baseline—what worked for corn might not work for their new batch of corn, which might have 1% more protein. Last year, a customer switched to organic corn from a new supplier, and his puffs were coming out smaller than usual. We tested the organic corn, found it had 14% moisture instead of his usual 12%, so we dried it a bit before loading, bumped the heating zone temp by 10°C, and his puffs were back to normal. No extra equipment, just adjusting for raw material changes.
Another common issue: over-adjusting. I’ve seen producers tweak parameters by 50 RPM, 20°C, or 10 bar in one go, and that sends the whole production line off track. Always make small, incremental changes: adjust screw speed by 25 RPM, barrel temp by 5°C, die pressure by 1 bar, and run a test batch between each change. That way, if your puffs get too airy after a 25 RPM bump, you can bring it back 25 RPM, instead of having to fix a whole batch of bad product. I once had a customer who was so eager to scale production, he bumped screw speed from 200 to 400 RPM in one step. The machine overheated, the die clogged, and he had to take the whole line apart for 8 hours to unclog it—cost him a full day of production, plus repair parts. He learned quickly that small changes are better than big, sudden ones.
Now, if you’re still stuck—if you’ve tweaked all the parameters, done test batches, and your puffs are still too dense, too airy, breaking, or soggy—don’t hesitate to reach out. As a puffed snacks processing machine supplier, we don’t just sell you equipment and leave you to figure it out. Our field techs work directly with producers to tune parameters for their specific products and raw materials, whether you’re making 100 kg a day or 10,000 kg a day. We also provide detailed parameter guides for different grain types and snack styles, so you don’t have to start from scratch. The key is that tuning isn’t a one-time task—you’ll need to adjust parameters every few days if your raw grain changes, or if you switch to a new snack recipe, or even if the weather changes and affects grain moisture. It’s a continuous process, but once you get the hang of it, it’s the difference between wasted batches and consistent, high-quality puffed snacks that keep your customers coming back.
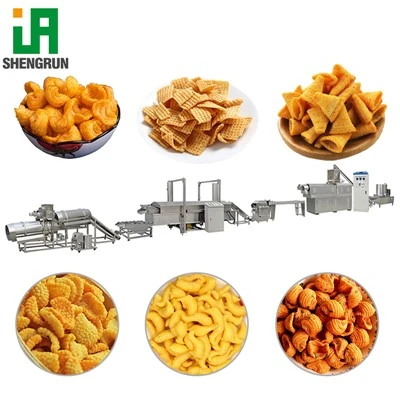
If you’re ready to get your parameters right, or you have questions about tuning your machine, we’re here to help. We work with producers of all sizes, from small artisanal brands to large manufacturing facilities, and we tailor our support to your needs. Don’t let confusing machine settings hold you back from making the puffed snacks you want. Reach out today to discuss your production goals, and we’ll walk you through every step of parameter adjustment to get you started.
Fish Feed Production Line References
- Tolaba, M. P., & Suárez, C. (2004). Extrusion cooking of corn: A review. Journal of Food Engineering, 64(1), 107-115.
- Brennan, J. G. (2012). Food Processing Handbook (2nd ed.). Wiley-Blackwell.
- Harper, J. M. (1981). Extrusion of Foods: Volume 1. CRC Press.
- Riaz, M. N. (2008). Extruders in Food Applications. CRC Press.
- Gomez, M. H., & Aguilera, J. M. (1983). A physicochemical model for extrusion of starchy materials. Journal of Food Science, 48(1), 106-111.
Jinan Shengrun Machinery Co., Ltd.
We are one of the most professional puffed snacks processing machine manufacturers and suppliers in China, featured by quality products and good price. Please rest assured to buy durable puffed snacks processing machine for sale here from our factory. Contact us for more details.
Address: 1817 Rongce Center, No.3179 Qilu Avenue, Xingfu Street, Huaiyin District, Jinan City, Shandong Province
E-mail: sales@foodgm.cn
WebSite: https://www.food-gm.com/
