Hey everyone, if you’ve ever worked with slant-bed CNC lathes—whether you’re a machinist, a shop foreman, or someone who’s just started digging into precision machining—you know there’s a lot going on under the hood that makes these machines way more reliable and accurate than their flat-bed cousins. Today, I’m gonna break down one of the unsung heroes of our slant-bed CNC lathes: the limit switch. Don’t roll your eyes yet—this tiny, often overlooked part is actually what keeps your machine from crashing, makes your parts dead-on, and saves you from a whole lot of headache (and expensive repairs). I’m Jake, and I’ve been supplying slant-bed CNC lathes to shops like yours for 12 years, so I’ve seen firsthand what happens when limit switches work… and when they don’t. Let’s get real about this. Slant-bed CNC Lathe

First off, let’s keep this simple. A limit switch is just a small electromechanical device that triggers a signal when something physically touches it—no fancy tech, no overcomplicating things. But on a slant-bed CNC lathe, its role is way more specific than just “stopping the machine.” Unlike a flat-bed lathe, where the cutting tool moves parallel to the bed in a more linear, less angled setup, slant-bed lathes have that angled bed (usually 30, 45, or 60 degrees) that lets chips fall away naturally, makes tool changes faster, and gives better chip control. That angle also puts more stress on the axes—your X-axis (the one moving left/right) and Z-axis (moving front/back) are working against gravity a lot more than on a flat bed, so the limit switches’ jobs are non-negotiable here.
Let’s start with the big one: preventing catastrophic crashes. I can’t tell you how many times a new customer calls me panicking because their lathe ran into a chuck, a tool holder, or the tailstock. When that happens, you’re looking at a bent ball screw, a cracked way cover, a broken tool—all of which cost thousands of dollars in parts and downtime, not to mention the time you lose on a big job. The limit switches are the last line of defense before that crash. Every axis has two of them: a hard limit and a soft limit? Wait, no—let me clarify: hard limits are the physical ones mounted at the extreme ends of the axis travel, and soft limits are set in the CNC control software, but the hard limit switch is what actually stops the machine when the soft limit is breached.
Here’s how that works. Let’s say you’re turning a long shaft, and you program the Z-axis to move 20 inches forward, but you accidentally type 200 inches instead (we’ve all been there, right? Fat fingers on the keypad). The soft limit set in the control is 150 inches for the Z-axis, so the machine would normally stop before hitting the end. But if the soft limit fails for some reason—like a glitch in the control or a misconfigured setting—the hard limit switch is there. When the Z-axis moves all the way forward and triggers that switch, it sends an immediate signal to the servo motor to cut power. No more movement. No crash. I had a customer last year who skipped a maintenance check because they were swamped with a rush order—their old lathe’s limit switch was dirty, so it didn’t trigger when the axis overrode the soft limit. They totaled a $800 tool holder and dented the chuck. With our lathes, we do a full limit switch test during pre-delivery, so that never happens. That’s the kind of thing that keeps shops running.
Next, positioning accuracy. Slant-bed CNC lathes are all about precision—we’re talking thousandths of an inch, because even a tiny error means a part gets scrapped. The limit switches aren’t just for stopping; they’re also used for homing the axes every time you power on the machine. Homing is when the machine finds its “zero point” so it knows exactly where every axis is in space. Here’s why that’s critical for slant-bed setups: because the bed is angled, gravity can cause the axes to drift a little when the machine is off. If you don’t home correctly, your first cut will be off. The limit switch acts as a fixed reference point—when the axis moves back to the switch, the control registers that as the home position, so every subsequent move is calculated from that exact spot. I’ve seen shops skip homing to save time, and they end up with parts that are 0.005 inches off. On a medical part or a aerospace component, that’s a failure. Our technicians always emphasize that homing using the limit switches is non-negotiable, even if it adds 30 seconds to the startup routine. It’s a small price to pay for consistent accuracy.
Then there’s tool change and part handling. A lot of modern slant-bed CNC lathes have automatic tool changers (ATCs), which hold multiple tools so you don’t have to stop and swap tools manually every time. The limit switches are what tell the ATC exactly where to grab the next tool—no misalignment, no dropping tools in the machine. If the tool turret moves past its intended position, the limit switch stops it before it crashes into the tool magazine or the spindle. We had a customer a while back who was running a batch of 50 brake caliper parts, and their old lathe’s ATC limit switch was worn out. The turret moved 10 degrees too far, knocked a tool into the spindle, and ruined all 50 parts. They replaced their lathe with one of ours the next week. On our machines, we use high-quality limit switches from brands that are built to handle constant, heavy use, so that kind of wear-and-tear failure is rare.
Wait, also—chip control. I mentioned earlier that slant-bed lathes throw chips away from the cutting zone, and the limit switches play a tiny role here too. The Z-axis limit switch is usually mounted towards the headstock, so when you’re turning a part close to the headstock, you don’t have to worry about chips piling up around the switch and messing with it. We design our limit switch enclosures to be sealed, so coolant and chips don’t get inside. That’s a big deal because if a switch gets gunked up with metal chips, it might not trigger when it’s supposed to, leading to all those crashes I talked about.
Now, let’s talk about common misconceptions. A lot of people think limit switches are “set it and forget it.” That’s the worst mistake you can make. Just like any other part on a CNC lathe, limit switches need regular checks. Over time, the actuator (the little arm that gets pressed when the axis moves) can wear out, the wires can get frayed from constant movement, or dust and chips can build up around it. We include a quick limit switch inspection checklist with every lathe we sell—things like checking that the actuator moves freely, testing the switch trigger, and making sure the wiring isn’t damaged. I always tell our customers to do this every 500 operating hours, or after a big job where they pushed the machine hard. Last quarter, a shop in Detroit called me because their limit switch was acting up, and when our tech got there, he found that the actuator pin was bent from a tool crash that hadn’t caused any obvious damage. If they hadn’t checked, the next time the soft limit failed, they would’ve had a way bigger problem.
Another thing: on slant-bed lathes, the weight distribution is different than flat-bed, so the limit switches have to handle different forces. The X-axis on a slant-bed lathe is working against gravity, so if the limit switch fails, the axis can creep forward when the machine is off, which throws off the home position. That’s not a problem with flat-bed machines, so a lot of shops that switch to slant-bed don’t realize they need to be more diligent about their limit switches. We train all our customers’ operators on that, because we want them to get the most out of their lathe.
Let’s wrap this up with why this matters for you. If you’re in the market for a slant-bed CNC lathe, you’re not just buying a machine that cuts metal—you’re buying a machine that runs all day, every day, with minimal downtime. The limit switch is a small part, but it’s integral to that reliability. We don’t cut corners on limit switches when we build our lathes—we use industrial-grade switches that are rated for thousands of operations, we seal them to keep out coolant and chips, and we test every single one before it leaves our facility.
If you’re currently having issues with your slant-bed lathe’s limit switches causing errors or crashes, don’t waste time troubleshooting old parts. A good limit switch setup can save you thousands in repairs, scrap parts, and downtime. I’ve been doing this for over a decade, and I’ve seen too many shops suffer because they ignored this tiny component. The slant-bed design is what makes our lathes stand out in terms of chip control and precision, but the limit switches are what make that design work day in and day out.
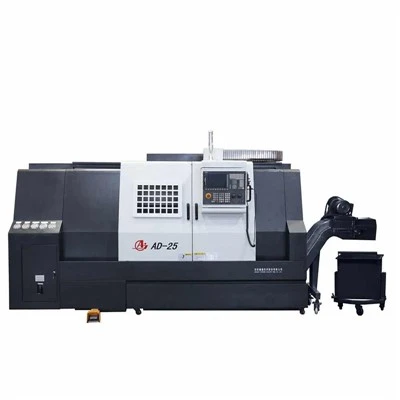
If you’re looking to upgrade your current setup or buy your first slant-bed CNC lathe, we’re here to help. We can walk you through the different models, show you how our limit switch systems are built to handle the demands of high-volume machining, and answer any questions you have. Don’t settle for a lathe that’s going to give you trouble because of overlooked parts—reach out to us, and we’ll make sure you get a machine that keeps your shop running smoothly.
Standard Turning Lathe References
- ABS, Guide to CNC Lathe Safety and Maintenance, 2022.
- Haas Automation, Slant-Bed vs Flat-Bed CNC Lathes: Key Differences, 2021.
- Panasonic Industrial Devices, Limit Switch Selection for Industrial Automation, 2020.
- Machining Dojo, Common CNC Lathe Crash Causes and Prevention, 2023.
Anyang Xinsheng Machine Tool Co., Ltd.
We’re well-known as one of the leading slant-bed cnc lathe manufacturers and suppliers in China, featured by quality products and good price. Please rest assured to buy advanced slant-bed cnc lathe made in China here from our factory. Contact us for more details.
Address: No.68 Renmin road, Anyang, Henan, China
E-mail: sales@anyangst.com
WebSite: https://www.xslathe.com/
